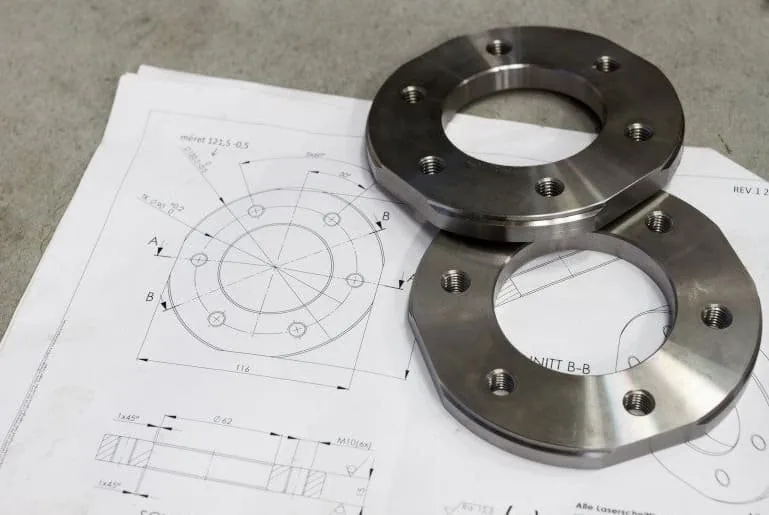
Quick answer: Put one general tolerance in the title block — ISO 2768-m covers most features — then tighten only the dimensions that control fit, sealing, alignment or motion. A drawing that calls ±0.01 mm everywhere looks safe and is not: it forces slower cutting, extra passes and more inspection on features where none of it changes how the part works. Say which dimensions matter and the quote usually comes down.
Two drawings can describe the same bracket and come back at noticeably different prices. The difference is rarely the material or the quantity. It is the tolerance block, and how much of the part the tight numbers cover.
Why a blanket tight tolerance costs more than it looks
A tolerance is not just a number on paper. It decides how fast the cutter runs, how many finishing passes the part needs, whether it has to be re-fixtured, and how long it spends on the inspection bench. A blanket tolerance applies all of that everywhere at once.
The expensive drawings are usually not the demanding ones. A print with three carefully chosen tight dimensions is cheaper to make than one where nobody decided which three mattered, so every dimension got the tight number.
The short version
| Feature | What usually works | Why |
|---|---|---|
| Bracket outlines, non-critical lengths | ISO 2768-m general tolerance | Nothing mates with them |
| Bolt clearance holes | General tolerance or a stated clearance fit | A tight hole buys nothing here |
| Bearing or bush seats | H7, or a stated press/slip fit | The dimension does real work |
| Sliding or guiding faces | Size plus form control | Size alone does not stop a face being curved |
| Sealing faces | Flatness plus a surface finish callout | Sealing is about flatness and texture |
| Datum and mounting features | Geometric tolerances tied to named datums | Controls how the part sits, not just its size |
Start from a general tolerance, then tighten selectively
ISO 2768-m is the general tolerance we work to unless a drawing says otherwise — close enough for brackets, housings and fixture bodies, and loose enough to machine at a normal pace.
From there, tighten only what has to be tight. On most parts that is a handful of dimensions — the bores that hold a shaft, the faces that seal, the hole pattern that lines up with the mating part. Everything else can stay on the general tolerance, and the difference shows up in the price.
If you are not sure which, describe what the part does and what it mates with — that is usually enough, and it is worth raising before the first part is cut.
Tight numbers earn their keep in four places: fits — a bearing seat, a press-fit pin, a bore that has to accept a shaft without play; sealing faces, where flatness and texture do the work rather than the overall thickness; alignment — hole patterns that line up across two parts; and motion — slides and guides that must move without binding. Those are the features where a tighter number, a form control or a finish callout changes how the assembly behaves.
Callouts that add cost without adding function
The other side of the same coin — these appear constantly and rarely change how the part performs:
| Common callout | What it costs | What to write instead |
|---|---|---|
| ±0.01 mm on every linear dimension | Slower cutting, extra passes and more inspection across the part | ISO 2768-m in the title block; ±0.01 mm only on fit dimensions |
| A fine Ra on faces that touch nothing | Extra finishing passes, more handling | Finish callout on sealing and sliding faces; rest as machined |
| Tight perpendicularity on a non-datum face | Extra setups, more CMM time | Form control only where it affects assembly |
| Sharp internal corners (R0 or unspecified) | Small cutters, many passes, slower cycles | The largest acceptable corner radius |
| Tight flatness at the bottom of a deep blind pocket | Special tooling and slow finishing | Relax the flatness, or make the pocket through |
To be clear, this is not an argument for sloppy parts — only for putting the precision where it does something.
Datums, GD&T, and what we actually check
Coordinate tolerances describe how big each feature is. They do not describe how the features relate to each other — that is what geometric tolerancing is for, and on parts with several machined faces it usually produces a clearer drawing than a page of ±values.
You do not need a full GD&T scheme to get the benefit. Three things do most of the work:
- Name your datums — the faces the part is measured and assembled from.
- Control form where form matters — flatness on a sealing face, perpendicularity on a mounting face, position on a hole pattern.
- Separate function from appearance — a face that must look flat and one that must seal are different requirements.
The drawing also tells us what to check. Fit-critical dimensions and any geometric callout are measured and can be reported; features on the general tolerance are controlled through the normal machining process. If you want a full dimensional report, ask when you request the quote — inspection reports are available on request, with material traceability — but measuring everything costs more than measuring what matters.
Five notes that cut cost without hurting function
- Allow the largest corner radius you can. Internal corners are cut with round tools; a stated radius lets us use a bigger, faster cutter.
- Say which faces are cosmetic. Then we know where a handling mark is a reject and where it is not.
- Avoid unnecessarily deep pockets. Depth drives tool reach, deflection and cycle time more than almost anything else.
- Standardise hole sizes across the part. Fewer tool changes, fewer setups.
- Give the quantity you actually need. Ten and three hundred are different jobs; quoting the real number avoids a re-quote later.
These are notes on a drawing that already exists. Tolerance and process are the same decision from two sides: tight, repeatable tolerances across a batch are usually held by finishing operations rather than by cutting slower — CNC grinding at ±0.002 mm, or wire EDM at ±0.01 mm and ±0.005 mm on high-precision work. Geometry matters just as much: a tight tolerance on a feature needing three setups costs more than the same tolerance reachable in one, which is where 5-axis machining pays for itself, while 3-axis milling and CNC turning stay cheapest where they work. Full ranges are on the CNC machining tolerances page.
Frequently asked questions
What tolerance should I put on the drawing if I am not sure?
Put ISO 2768-m in the title block as the general tolerance, then mark the dimensions that genuinely control a fit, a seal or an alignment. If you are unsure which, describe how the part assembles. Leaving the tight number off by default is the cheaper mistake.
Does a tighter tolerance mean a better part?
Not by itself. A tighter tolerance means a more expensive part that takes longer to make. It is better only when the dimension does something — holds a bearing, seals a face, lines up a hole pattern.
Can you hold ±0.01 mm on my part?
On fit-critical features, yes — ±0.01 mm is routine where a drawing calls for it. Grinding covers tighter work to ±0.002 mm and wire EDM holds ±0.005 mm on high-precision profiles. Send the drawing and we will confirm what is practical on each dimension.
Do you inspect every dimension on every part?
Fit-critical dimensions and any geometric callout are measured and can be reported. Features on the general tolerance are controlled through the normal machining process. A full dimensional report covering every feature is available on request.
Should I use GD&T or coordinate tolerances?
For simple parts, coordinate tolerances with a general note are fine. Once several machined faces have to relate to each other, GD&T is usually clearer and often cheaper, because it states what must be controlled. At minimum, name your datums.
What should I send to get a quote?
A STEP or IGES model plus a dimensioned PDF, the material, the quantity and your target date. If the drawing has a tolerance block, include it. We review every drawing before quoting, and if we see a feature that cannot be machined as drawn, or one that adds cost without adding function, we point it out and suggest an alternative for you to confirm.
Send the drawing
Send a STEP, IGES or DWG model with a dimensioned PDF, the material, the quantity and your target date. If you are not sure which tolerances the part needs, say what it has to mate with and how it has to move — that is enough to work from. Standard lead time is 2–4 weeks. Rush orders are confirmed case by case. You get a priced quote within 48 hours in the normal case, with tolerance and lead time stated on it. Parts ship from Guangdong. Material choice shifts the numbers more than most expect — aluminium, stainless steel and titanium each respond differently to a tight callout. For one-off prototypes or repeat automation parts, start on the contact page.