CNC Machining Brass & Copper
Fast, clean machining of C360 brass, C110 copper and beryllium copper — for fittings, connectors, bus bars and heat-transfer parts where conductivity or machinability drives the design.
- C360 cuts 2–3× faster than steel
- Ra 0.8 µm as-machined finish
- Plating and polishing available
Quick answer
Brass and copper are the fastest, cleanest metals to machine. Brass cuts at roughly two to three times the speed of mild steel, produces short chips that clear easily, and holds a fine surface finish straight off the tool — which is why it is still the default for precision turned fittings, connectors and valve bodies. Copper is softer and gummier, harder to machine well, but unmatched when you need electrical or thermal conductivity.
We quote brass and copper work within 48 hours in the normal case and machine it on the same equipment as milling, turning and 5-axis jobs, with plating and passivation available afterwards.
Common grades and when to use them
C360 is the default where the function allows it — nothing else machines as cheaply.
| Grade | Composition | Machinability | Best for |
|---|---|---|---|
| C36000 (C360) | Free-cutting brass, ~3% lead | Excellent — the benchmark, rated 100% | Fittings, connectors, valve bodies, screw machine parts |
| C38500 | Architectural brass | Very good | Extruded sections, decorative hardware |
| C46400 | Naval brass | Good | Marine hardware, condenser plates |
| C26000 | Cartridge brass, 70/30 | Fair — gummier than C360 | Formed parts, radiators, ammunition components |
| C11000 | Electrolytic tough pitch copper, 99.9% | Poor — soft and gummy | Bus bars, electrical contacts, heat sinks |
| C10100 | Oxygen-free copper | Poor | Vacuum and electronics where conductivity is critical |
| C17200 | Beryllium copper | Good before heat treatment | Springs, contacts, non-sparking tools |
| C93200 | Bearing bronze | Good | Bushings, wear plates |
Properties that affect your design
Copper conducts roughly three times better than brass and costs more to machine — pick on function, not habit.
| Property | C360 brass | C110 copper |
|---|---|---|
| Machinability rating | 100% (reference) | 20% |
| Tensile strength | ~340 – 470 MPa | ~210 – 240 MPa (annealed) |
| Thermal conductivity | ~115 W/m·K | ~390 W/m·K |
| Electrical conductivity | ~26% IACS | ~100% IACS |
| Density | 8.5 g/cm³ | 8.9 g/cm³ |
| Corrosion resistance | Good; dezincification risk in some environments | Good; develops a protective patina |
| Magnetic | No | No |
| Relative material cost | Moderate | High |
Machining Capability
What we hold on brass and copper parts.
Tolerances
±0.01 mm
ISO 2768-m standard; ±0.005 mm achievable on critical features.
Surface Finish
Ra 0.8 µm
Routinely as machined; Ra 0.4 µm with fine passes.
Processes
Turn · Mill · 5-axis
Plus drilling, tapping and knurling.
Work Envelope
Up to 1000 mm
Bar work up to 65 mm diameter on turning.
Finishing
Ni · Cr · Sn · Polish
Plating, polishing, passivation and lacquer available.
Lead Time
2 – 4 weeks
Faster for simple turned parts in C360.
Design tips for brass and copper
Most cost savings here come from grade choice and realistic tolerances.
- Choose C360 when the part is machined. If the function allows it, C360 is dramatically cheaper per part than C260 or copper, because cycle time drops and tool life rises.
- Copper needs sharp tools and high rake. Expect slower feeds and a higher price than the same geometry in brass — avoid deep, narrow pockets in copper.
- Watch thin walls on copper. It is soft and deflects under cutting pressure; keep wall thickness above 1 mm where possible.
- Specify dezincification-resistant brass for water contact. Standard brass can leach zinc in certain water chemistries — tell us the service environment.
- Plating changes dimensions. If a thread or bore must fit after plating, state the post-plating size and we will machine to suit.
- Copper work-hardens if rubbed. Avoid very light finishing passes — a proper chip load gives a better surface than a rubbing tool.
- Use brass for threads in soft assemblies. Brass threads gall far less than stainless and do not need anti-seize.
- Consider bronze for wear components such as bushings, where bearing behaviour matters more than machinability.
Finishing and appearance
Brass machines to a bright, clean surface that many customers use as-is. Where the environment or the appearance demands more, the usual options are nickel plating (hard, bright and corrosion resistant — the standard choice for engineering components), chrome plating (decorative and very hard wearing, usually over a nickel base), tin plating (common on electrical parts, improves solderability), polishing and buffing (practical on machined brass because the as-cut finish is already fine), and lacquer or passivation to slow tarnishing on handled or displayed parts.
Plating adds thickness. If a bore, thread or mating face must be a specific size after plating, state the finished dimension and we will machine to suit. See surface finishes for the full list.
Frequently Asked Questions
Answers to the questions we get asked most about this process.
Why is brass more expensive per kg than steel but often cheaper per part?
Machining time dominates cost on small precision parts. Brass cuts two to three times faster than steel, tool life is longer, and it usually needs no finishing operation. The part often ends up cheaper even though the raw stock costs more.
Is C360 brass safe for drinking water components?
C360 contains lead and is not compliant with lead-free plumbing regulations in many markets. For potable water, ask about lead-free alternatives such as C69300 or the silicon bronzes and we will advise on the relevant standard for your market.
Can you machine beryllium copper?
Yes in the annealed or solution-treated condition. Machining dust from beryllium alloys requires controlled handling, so we confirm the condition and any safety requirements before quoting.
How does copper compare with aluminium for heat sinks?
Copper conducts roughly twice as well, but it is three times denser and much slower to machine. Aluminium fins are usually the better value; copper makes sense for spreader plates and heat pipes where volume is limited. See our aluminium grade comparison for the aluminium side of the trade-off.
Do you provide material certificates and inspection reports?
Material certificates come with the stock from the supplier and can be supplied with your order. Dimensional inspection reports are available on request.
Can you plate the parts after machining?
Yes. Nickel, chrome, tin and passivation are all arranged as part of the job. Tell us the finished dimension if plating thickness affects a fit — see surface finishes.
Typical applications
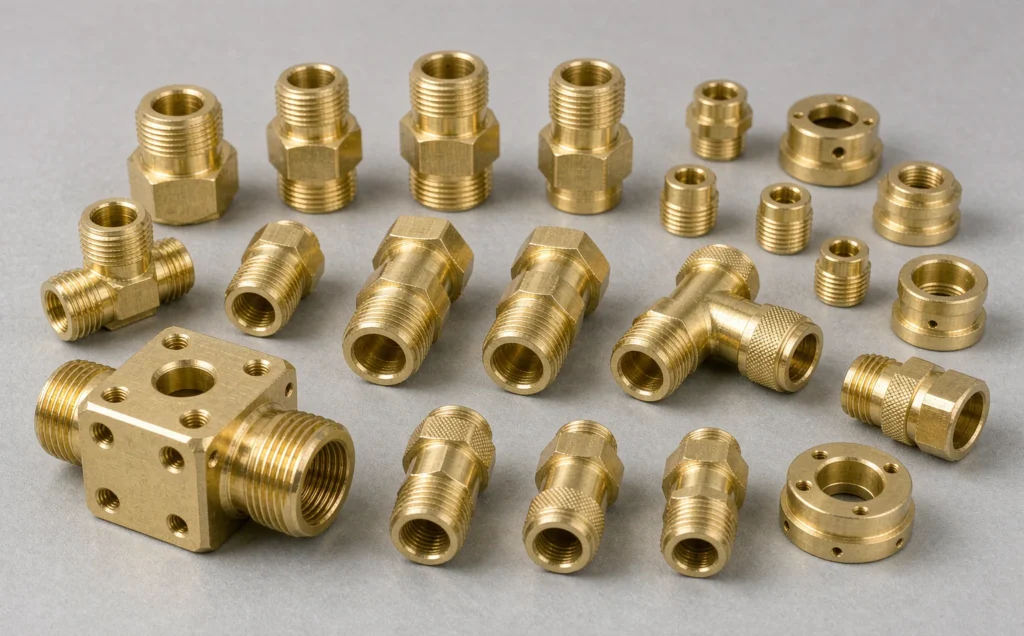
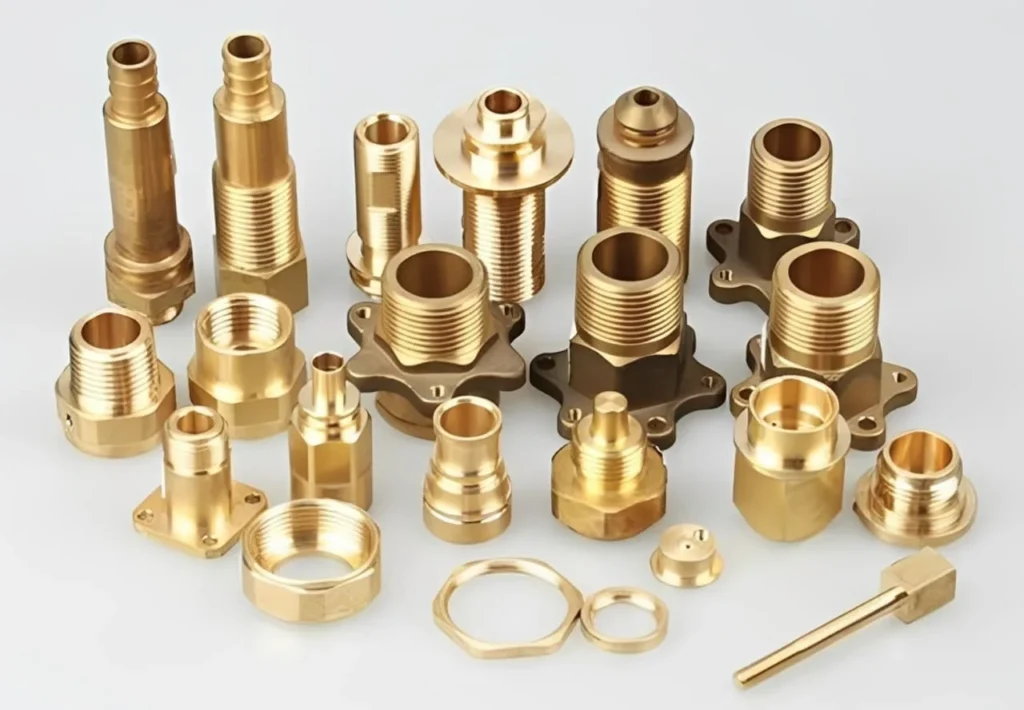
Pneumatic and hydraulic fittings, electrical connectors and terminals, bus bars and current-carrying hardware, valve bodies and manifolds, precision turned spacers and standoffs, decorative hardware with polished or plated finishes, and wear components such as bushings where bronze may be the better choice.
The two families of enquiry we see most are fluid fittings — where C360 machinability and natural galling resistance make it the default — and electrical hardware, where copper or C110 is chosen for conductivity and brass for everything around it. If your part does both, tell us which function is critical and we will recommend the grade rather than defaulting to whichever is easier to machine.
Ready to Start Your Project?
Send drawings in STEP, IGES or DWG. You get a priced quote within 48 hours in the normal case, with tolerance and lead time stated up front.